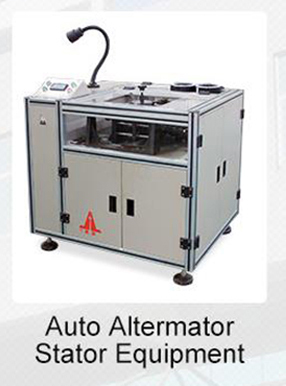
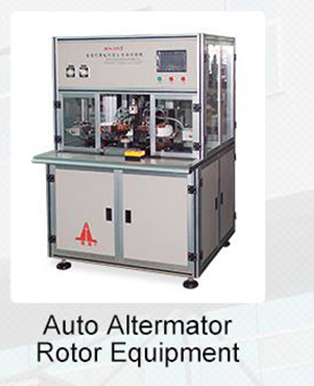
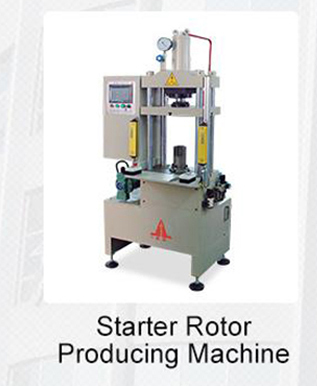
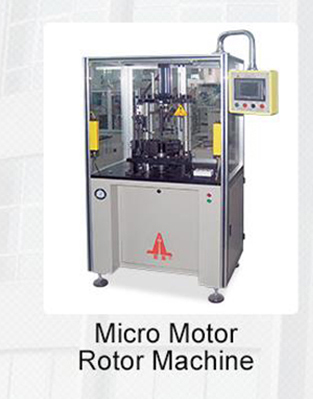
Automatic Stator Wire Winding Machine
- KinematicsDual-flyer / Servo indexing
- Wire Diameter0.18 mm – 1.60 mm
- Stack Height15 mm – 180 mm
- Control SystemIndustrial CNC Touchscreen
Direct manufacturer in Sanmen, Zhejiang
Rigorous QA and full FAT verification
Proprietary kinematics and custom tooling
FOB / CFR / CIF / EXW · Dedicated support
In electric vehicle traction, industrial automation, brushless DC (BLDC) systems, and household appliances, stator efficiency directly dictates overall electromechanical performance. As slot fill factor requirements surpass 75% and thermal limits tighten, manual or semi-automated winding methods introduce enamel damage, erratic slot positioning, uneven phase resistance, and unacceptable scrap rates.
Explore our flagship configurations developed for automotive starters, alternators, industrial drive units, submersible pumps, and BLDC brushless motor lines.
Compare standard parameters across our core stator manufacturing and coil winding platforms.
| Machine Model | Primary Stator Architecture | Wire Gauge Capacity | Typical Cycle Time | Slot Indexing Mechanism | Recommended Line Pairing |
|---|---|---|---|---|---|
| DB-5C Automatic Winder | Universal 2-Pole to 48-Pole Stators | 0.18 mm to 1.60 mm (Round) | 12 – 40 sec / pole group | Harmonic Servo Reducer (±0.01°) | DQ-1 Wire Embedding Machine |
| DQ-1 Stator Embedding | Slotted Internal Laminations | Multi-strand bundle compatible | 8 – 16 sec / core | Linear Cam + Servo Ram | DFC-1 Wedge Paper Inserter |
| 4-BL-1 Wave Winder | Alternator & Heavy Traction Stators | 0.80 mm to 2.20 mm enameled | Continuous multi-tooth wave | Synchronous Electronic Cam | 5-SC-2B Flat Wire Shaper |
| 1-QR-2 Field Coil Winder | Magnetic Pole Shoes & Field Coils | Heavy square / round copper | 15 – 35 sec / pole | Rotary Indexing Chuck | SDZ-120B Spot Welder |
| DFC-1 Wedge Inserter | Automotive & Industrial Alternator Stators | DMD, Nomex, Polyester films | 0.3 – 0.5 sec / slot | Rotary Pneumatic / Stepper Index | DQ-226/100 Trickle Impregnation |
A high-performance stator winding machine performs best when fully synchronized with upstream slot insulation and downstream lacing, shaping, and trickling operations.
Slot liner paper or Nomex/DMD composite is precisely cut, cuffed, and inserted into stator slots using horizontal or vertical slot insulating equipment, eliminating edge creepage.
Using the DB-5C automatic stator wire winder, enameled wire is wound either directly into open slots or transferred through high-speed continuous flyer tooling to transfer cassettes.
The DQ-1 Stator Wire Embedding Machine simultaneously drives coil bundles and insulating slot wedges into closed or semi-closed slots without scraping or over-straining magnet wires.
Coil overhangs are formed using 3D hydraulic intermediate and final shaping presses, followed by void-free resin trickling in our DQ-226 automated horizontal impregnation systems.
As electric motor specifications transition under global efficiency mandates (IE4/IE5 and premium automotive OEM targets), procurement teams must balance cycle efficiency against tooling flexibility.
Clear, engineering-grounded answers addressing the specific criteria international motor manufacturers evaluate during machine selection.
Protecting wire enamel requires controlling both dynamic kinetic friction and instantaneous tension spikes. Zhejiang Rilvo Automation Equipment Co., Ltd. equips every machine with mirror-polished zirconia-ceramic wire guides, molybdenum-treated rolling sheaves, and closed-loop electronic tension controllers. When the machine accelerates during rapid indexing, the servo-controlled unwinding system dynamically matches wire feed rates, ensuring wire tension stays within ±1.5% of setpoint and eliminating dielectric breakdown or microscopic insulation cracks.
Needle winding utilizes a hollow needle delivering wire directly into the internal slots of segmented or concentrated BLDC stators, providing superior copper packing for brushless motors. Flyer winding utilizes high-speed rotating flyer arms to deposit wire onto external transfer tooling or rotating formers. Transfer embedding (using machines like our DQ-1) winds coils on separate tooling forms first, then pushes coils and insulating slot wedges into deep semi-enclosed AC stator slots simultaneously. Rilvo manufactures all three types to best match your motor lamination design.
For identical stator diameters with varying stack heights (for example, stepping from 35 mm to 65 mm), changeover is 100% digital and takes under 5 minutes by calling up pre-programmed recipes in our touchscreen PLC. When changing stator outside diameter (OD), inside diameter (ID), or slot numbers, modular quick-release cassette tooling allows an operator to replace the winding nozzles, guide shrouds, and clamping jaws in 30 to 45 minutes without recalibrating kinematic zero points.
To provide an exact machine configuration and cycle time estimate, our 36 R&D engineers request: (1) Stator 2D/3D drawings showing stack height, inner/outer diameter, slot geometry, and insulation thickness; (2) Wire diameter (swg/awg/mm), strand count, and insulation thermal rating (Grade 1/2, Class H/N); (3) Winding scheme (slot pitch, turns per pole, star/delta connections); and (4) Desired production capacity per 8-hour shift.
Before shipment, we run extensive trials on our assembly floor using your supplied lamination cores and magnet wire. We perform insulation surge tests, winding resistance symmetry checks, and high-speed video recording for remote FAT sign-off. Post-delivery, we supply complete bilingual documentation, CAD schematics, and interactive video guidance. We also dispatch experienced field engineers worldwide to conduct on-site line commissioning, operator training, and process optimization.
Founded in 1998, Zhejiang Rilvo Automation Equipment Co., Ltd. has established itself as an authoritative manufacturer and engineering solution provider in the global motor manufacturing industry. We specialize in the R&D and production of micro-motor manufacturing equipment, stator and rotor automatic winding machines, special welding apparatus, electric bicycle manufacturing and testing lines, electronic component assembly machines, and electrostatic powder spraying lines.
Recognized as an official High and New Technology Enterprise of Zhejiang Province, our manufacturing campus in the Shatianyang Development Zone of Sanmen encompasses nearly 60,000 square meters of land, with over 20,000 square meters of advanced workshop facilities and 30,000 square meters in secondary expansion. Our operations are governed under the ISO9001 Quality Management System and China Compulsory Certification (3C).
Full vertical integration ensures precision. From raw casting heat-treatment and CNC 5-axis machining to precision spindle grinding and final assembly, our manufacturing tolerances are maintained in-house without reliance on third-party subcontractors.
Years of Engineering Excellence
Manufacturing Base Area
Specialized Machine Models
In-House Machining Units
Registered National Patents
Heavy-duty meehanite cast-iron machine frames are stress-relieved to prevent thermal deformation and micro-vibrations during 3,000+ RPM flyer winding cycles.
Critical winding needles, flyer guide tooling, and stator clamping fixtures are machined on ultra-precision CNC centers to hold coaxiality within 0.005 mm.
Every automated winding axis is subjected to continuous multi-hour dry cycle runs, load testing, and optical backlash measurements in accordance with ISO9001 standards.
We wind your supplied motor laminations under real production parameters, validating slot fill factor, phase balance, surge test resistance, and overall cycle time before shipment approval.
Zhejiang Rilvo Automation Equipment Co., Ltd. satisfies strict international standards for equipment safety, electrical compliance, and operational reliability.
Audited Quality Management
China Compulsory Conformity
Zhejiang Provincial Recognition
Proprietary Kinematics & Tooling
Independent Physical Audit
Provide our engineering team with your stator lamination parameters, wire dimensions, and target shift output. We will analyze your slot topology and prepare a comprehensive turnkey proposal, tooling design, and cycle time calculation.