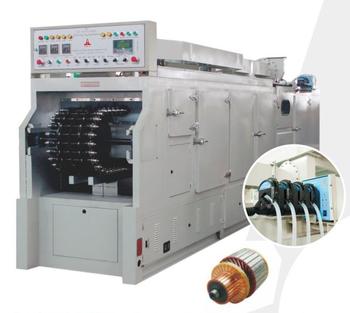
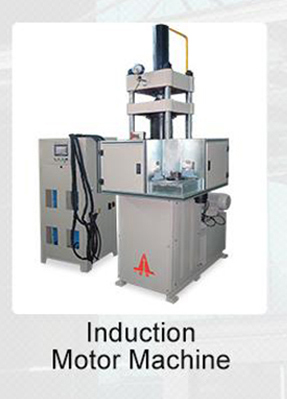
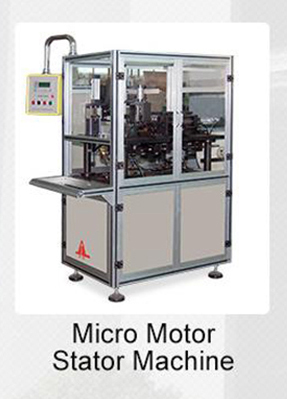
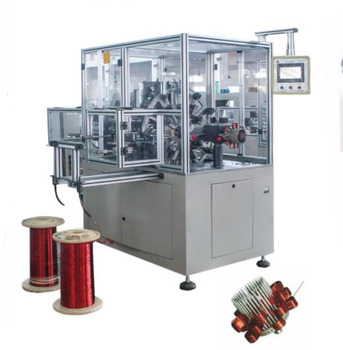
Automatic Stator Wire Winding Machine
- ApplicationStator Coil Winding
- ControlMulti-Axis CNC
- Line FunctionCell A Station
Proprietary machinery park in Zhejiang
Verified international quality control
Bespoke kinematics & tooling OEM/ODM
FOB / CIF turnkey line commissioning
Global procurement teams and manufacturing engineers face mounting pressure to navigate shifting motor architectures, tightening cycle-time mandates, and zero-defect quality thresholds. Below is an exhaustive technical breakdown for configuring high-yield automated motor assembly plants.
In modern industrial powertrain manufacturing, a Motor Total Assembly Line is far more than a linked chain of independent workstations; it is a synchronized cyber-physical system designed to integrate high-speed lamination handling, coil insertion, multi-axis commutator welding, precision rotor balancing, trickle impregnation, press-fitting, and full-spectrum End-of-Line (EOL) testing under unified SCADA/MES supervision. Whether manufacturing high-torque starter motors, compact brushless DC (BLDC) actuators, micro-motors, or e-mobility drive units, every assembly line must solve three fundamental mechanical conflicts: cycle time versus thermal stabilization during varnishing, mechanical positioning precision versus rapid tooling changeover, and high press forces versus core lamination damage.
A high-yield turnkey assembly line is typically segmented into three coordinated cells linked through asynchronous pallet-transfer conveyors with RFID-encoded workpiece tracking:
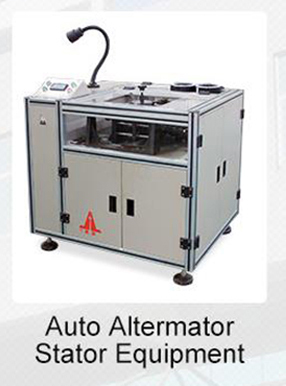
Handles slot insulation paper inserting, multi-strand winding, needle or flyer coil insertion, phase insulation, intermediate expanding, CNC lace lacing, and 3D terminal wire shaping. Precision servo positioning ensures minimal slot fullness enamel abrasion.
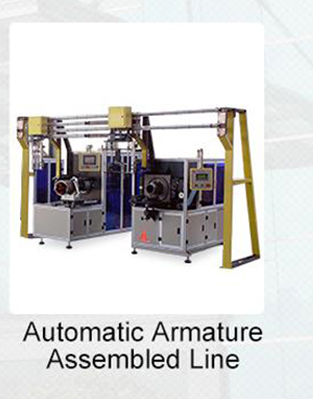
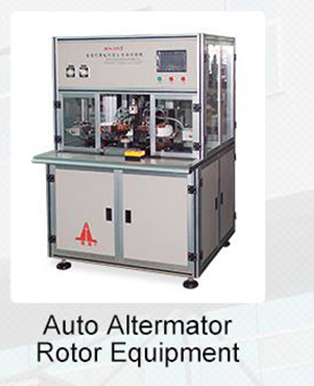
Executes shaft press-fitting with continuous force-stroke monitoring, armature lamination stacking, commutator pressing, precision multi-point spot welding/hot staking, automatic dynamic balancing (double-plane milling or drilling), and magnet positioning.
Coordinates trickle impregnation or oven curing, bearing press-fit, stator-rotor air gap insertion, housing shrink-fitting, brush-plate/encoder fastening, tie-rod screw driving, followed by 100% automated electrical and NVH functional testing.
Optimizing Capital Expenditure (CAPEX) vs. Operational Expenditure (OPEX) requires matching core machinery to specific motor topologies. Below is Zhejiang Rilvo Automation Equipment Co., Ltd.'s reference specification guideline for high-efficiency line planning:
| Assembly Module | Recommended Machine Model | Key Technical Parameters | Quality & Defect Prevention Target |
|---|---|---|---|
| Stator Wire Insertion | DQ-1 Stator Embedding Unit | Hydraulic / Servo push; cycle < 15s; slot fill > 78% | Zero enamel scrape; slot paper wrinkle prevention |
| Wedge Paper Forming | DFC-1 Horizontal Inserter | Step-motor indexing; variable edge fold; edge height ±0.2mm | Dielectric breakdown > 2.5 kV / 50 Hz |
| Rotor Winding | ZB-303 Three-Servo Winder | Triple-servo synchronized flyer; speed up to 3,000 RPM | Uniform coil resistance balance < 1.0% variation |
| Commutator Joining | SDZ-120B Intelligent Welder | Hot-staking inverter / capacitor discharge; microsecond feedback | Residual contact drop < 0.5 mV; zero burnt wire |
| Trickle Impregnation | DQ-226/100 Trickle System | PID controlled preheating; precision peristaltic resin delivery | 100% void-free slot penetration; class H thermal class |
| Permanent Magnet Handling | CT-40 Automatic Inserter | Pneumatic-servo guide; polar orientation verification | Magnetic flux polarity 100% verified; zero chipped magnets |
Industrial drives and automotive traction are transitioning rapidly away from conventional round-wire pull-in stators toward flat copper wire (hairpin) and continuous wave windings. Sourcing managers are increasingly specifying assembly lines with modular CNC flat-wire shaping, automated 3D slot populating, and laser-assisted twisted-end stripping to achieve copper slot fill rates exceeding 85%.
Procuring turnkey production lines without prior kinematics simulation is becoming obsolete. Leading overseas buyers now insist on comprehensive virtual commissioning (using PLC simulation suites) prior to mechanical cutting. This cuts on-site installation and SAT debugging cycles by over 45%, mitigating costly physical layout revisions.
Tier-1 automotive audits demand individual motor traceability. Next-generation assembly systems log every fastener's angle-torque curve, rotor balancing residual unbalance (mg·mm), surge test peak curves, and varnishing gel times directly into client cloud databases using OPC-UA industrial protocols.
As electric motor designs achieve extreme power densities (often exceeding 15 kW/kg in automotive and aerospace fields), motor assembly lines are adopting several disruptive process integrations:
Every automated assembly line designed by Zhejiang Rilvo Automation Equipment Co., Ltd. is engineered around your product drawings, cycle targets, and factory footprint.
Continuous insulation paper slotting, servo wire embedding, and automated intermediate wedge forming engineered for maximum copper slot filling with zero enamel stress.


High-torque armature winding, flat copper wire bar forming, dynamic balancing and closed-loop intelligent hot-stake resistance spot welding.


A motor total assembly line requires tight synergy across mechanical structure, electrical synchronization, and factory floor logistics. Zhejiang Rilvo Automation Equipment Co., Ltd. provides comprehensive in-house delivery.
Direct technical consultation for overseas line projects
Logistically positioned near Ningbo Port (under 2 hours), ensuring swift containerized dispatch worldwide.
Unlike trading assemblers who outsource critical tooling, Zhejiang Rilvo Automation Equipment Co., Ltd. machines, programs, assembles, and tests every module in-house to protect strict geometric and kinematic tolerances.
Years Automation Mastery
Factory Site Area
Standard Line Formats
Precision CNC Machining Units
National Invention Patents


Rigorous metallurgical, dimensional, and functional qualification for imported servomotors, linear guides, pneumatic systems, and precision sensors.
Critical winding flyers, lamination dies, and insertion tooling are crafted in-house to achieve sub-micron tolerances and extended service lives.
Complete pre-assembly dry cycles validating multi-axis servo trajectory, tension repeatability, cycle duration, and safety interlocks under ISO9001 protocols.
Continuous runs exceeding hundreds of actual workpiece samples to benchmark CPK > 1.67 across dimensional, resistance, and welding parameters before dispatch.


Zhejiang Rilvo Automation Equipment Co., Ltd. is a recognized high-tech enterprise focusing on research, development, and turnkey manufacturing of micro-motor manufacturing equipment, stator and rotor automation, special resistance welding systems, electric bicycle assembly and testing equipment, and complete electrostatic powder coating lines.
Recognised as a High and New Technology Enterprise of Zhejiang Province, our enterprise holds 17 national patents and strictly complies with ISO9001 quality management guidelines and China Compulsory Certification (3C). Our state-of-the-art campus located in the Shatianyang Development Zone of Sanmen encompasses nearly 60,000 m², boasting 20,000 m² of modern heavy-machinery workshops with an ongoing 30,000 m² phase advancement.
Our automation credentials, credit ratings, and export quality processes have been validated by on-site audits and international testing authorities.
Standardized Quality Management
China Compulsory Certification
Zhejiang Provincial Honor
Proprietary Kinematic Patents
Third-Party Field Audited
Clear, unvarnished technical answers addressing the critical queries plant directors and global sourcing managers formulate when evaluating motor assembly line vendors.
A turnkey motor total assembly line covers the entire automated sequence: stator processing (paper insertion, winding, inserting, shaping, tying), rotor sub-assembly (shaft press-fitting, dynamic balancing, commutator welding/hot staking), intermediate trickle impregnation or varnishing, marriage into the motor frame, bearing installation, end-bracket bolting, and automated End-of-Line (EOL) testing (dielectric withstand, insulation resistance, surge testing, partial discharge, and no-load/load characteristic analysis).
We deploy closed-loop servo feedback on all kinematic axes, load-cell force/displacement monitoring for every press-fit (ensuring interference tolerances without core buckling), machine vision verification for wire positioning and polar alignment, and full digital traceability via RFID-enabled pallets connected to an industrial MES layer that rejects non-conforming parts at intermediate diverter spurs.
Yes. Zhejiang Rilvo Automation Equipment Co., Ltd. incorporates modular tooling blocks, digital recipe management via multi-language HMIs, quick-release pneumatic locks, and universal adjustable pallet nests. Typical model changeovers (e.g., varying stator stack height or shaft diameter) are completed within 15 minutes without recalibration.
Standard design, manufacturing, and integration lead time spans 12 to 20 weeks depending on customization depth. We conduct a formal Factory Acceptance Test (FAT) with client parts at our 60,000 m² Sanmen plant, verifying CPK > 1.67 and target OEE > 88%, followed by full on-site Site Acceptance Testing (SAT) and fine-tuning by our dispatch engineering staff.
We supply comprehensive technical dossiers (3D exploded diagrams, electrical diagrams, spare part numbers), remote diagnostic VPN gateways for instantaneous troubleshooting, and dispatch experienced deployment engineers to your plant to oversee anchoring, electrical connection, and operator training until target shift output is reached.
Provide your motor stack height, rotor diameter, cycle time target, and degree of automation. Our technical team will generate a tailored line layout, cycle calculation, and quotation within 24 hours.