



Commutator Fusing
SDN-32ZH Commutator Fusing Machine
Hot-stake resistance fusing engineered for repeatable solid copper compacting, precise thermal energy monitoring, and continuous duty cycles.
Engineered to deliver tight copper wire slot fill factors, minimal enamel abrasion, and low cycle times for high-volume automotive starter motors and heavy industrial rotating machinery.
Hot-stake resistance fusing engineered for repeatable solid copper compacting, precise thermal energy monitoring, and continuous duty cycles.

Integrated multi-axis winder built for balanced dynamic flyer rotation, programmable turn tensioning, and low coil head build-up profiles.

Configured for versatile series motor and heavy-duty tool rotors, delivering uniform tension distribution across high slot count armatures.

Ultra-precision commutator surface finishing lathe. Guarantees sub-micron TIR concentricity and burr-free mica undercut edges.

Simultaneous servo insertion of enameled magnet wire arrays and slot insulation wedges without strand crossing or insulation scuffing.

Hardened tungsten alloy push blades, guide teeth, and custom wedge guide magazines calibrated to OEM stator lamination profiles.

Economical and robust spot welding station for stator lead tabs, brush card junctions, and ground terminal assembly blocks.

High-speed dual-station flyer head coil winding system engineered for multi-strand winding clusters and high-density industrial stator packs.
Automotive starters and auxiliary drive motors deployed across Texas must withstand intense thermo-mechanical stress, high ambient operational heat, and frequent rapid start cycles. Achieving flawless longevity begins in the primary manufacturing line where winding tension, insulation integrity, and copper compaction dictate the operational lifespan of rotating equipment.
Our automated production solutions eliminate intermittent insulation degradation through closed-loop servo-driven flyer tensioners and ultra-smooth coil guides. By reducing mechanical stretching of enamelled copper wire and guaranteeing precise slot wedge creepage distances, our machinery produces stator assemblies with exceptionally low partial discharge rates and superior thermal dissipation properties.
Whether producing heavy-duty commercial vehicle 24V starter field coils, hairpin flat-wire configurations, or precision fractional horsepower brushless actuators, our modular integration provides high machine availability (OEE > 88%) and complete production traceability from bare lamination stacking to post-trickle varnishing.
From Tier-1 automotive assembly centers in Arlington to defense manufacturing corridors in Grand Prairie and high-density electrification projects in North Texas, our equipment supports critical regional operations.
Supplying Tier-1 and remanufacturing plants across Arlington and Denton with automated line cells for 12V/24V high-torque starter armatures, alternator wave windings, and auxiliary EPS actuators built to endure intense highway heat cycles.
Serving precision motor contractors throughout Fort Worth and Grand Prairie with high-specification winding and testing solutions for extreme-environment starter-generators, actuator armatures, and military-grade auxiliary drives.
Engineering robust stator coil winding and trickle impregnation lines for heavy-duty electric submersible pumps (ESP), compressor motors, and rig auxiliary power units serving the broader Texas and Permian Basin energy corridor.
Strategic advancements in electrification, onshore component manufacturing, and smart line data collection driving machine capital investments across the Dallas industrial market.
Texas facilities are increasingly expanding internal automation to re-shore critical starter motor rebuilding and OE production. By transitioning from labor-intensive manual operations to high-precision semi-automatic winders and fusing systems, local shops offset regional wage pressures while achieving ISO-compliant quality standards.
Modern starter motors and alternator packages demand superior power density in compact frames. Achieving higher slot fill factors requires exact wire layering, zero-crossing flyer paths, and automated wedge folding that prevent copper pinching and ensure reliable high-heat heat transfer in confined engine bays.
Procurement teams in North Texas are mandating real-time process monitoring. Our stations integrate linear displacement transducers, welding current limit alarms, and optical inspection cameras to catch loose wire loops, cracked commutator bars, or insulation tears before parts advance downstream.
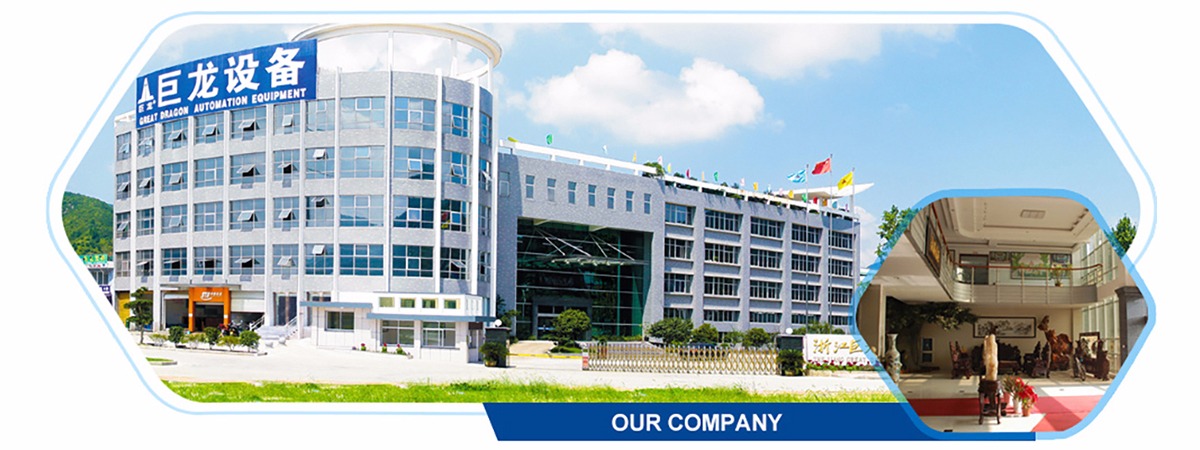
Founded in 1998, Zhejiang Rilvo Automation Equipment Co., Ltd. operates a comprehensive 60,000 m² campus in the Shatianyang Development Zone of Sanmen. Unlike commercial aggregators, every frame, winding nozzle, insertion guide, and electrical cabinet is designed, machined, and validated directly in our own facilities.
Led by our chief engineer—honored nationally for contributions to electromechanical innovation—our 36-member technical R&D department collaborates closely with automotive component makers to customize tooling according to exact stator lamination geometries, slot shapes, and cycle time demands.

Comprehensive technical and commercial answers addressing voltage compatibility, tooling turnaround, and overseas freight logistics.
Yes. All machines built for shipment to Texas or North American facilities are engineered with standard North American 480V, 240V, or 208V 3-phase 60Hz electrical systems. Controls feature international standard Schneider, Omron, or Mitsubishi PLC components with English HMI touchscreens, safety interlocks, and standardized NFPA-compliant wire routing schemas.
Yes. Custom engineering accounts for over 70% of our global export orders. Simply provide your core stack CAD drawings (.STEP/.DWG), lamination slot profiles, copper wire gauges, and expected target takt times. Our 36-member R&D engineering team will design custom winding flyers, inserting blades, wedge magazines, and fusing collets precisely tuned to your part envelope.
We mandate physical sample trials before container loading. Clients provide sample laminations, wire coils, and commutator shafts. We complete full trial batch runs, measuring slot resistance balance, weld shear strengths, and mechanical runouts. Complete video documentation, high-resolution microscope metallurgical images, and CMM dimension reports are submitted for formal sign-off before dispatch.
Standard standalone equipment typically ships within 30 to 45 business days, while customized multi-station automatic production lines require 60 to 90 days. Shipments dispatch from Ningbo Port (located approximately 2 hours from our factory) directly to the Port of Houston or Dallas rail inland ports (BNSF/UP logistics yards) under FOB, CIF, or DDP Incoterms.
Every machine is delivered with comprehensive electrical schematics, full wear-part lists, and pre-packaged consumable tooling (including winding nozzles, tungsten electrodes, and insertion pushers). Remote troubleshooting is supported through direct engineer-to-engineer video conference calls and integrated remote PLC diagnostic modules. Field service engineers can also be deployed to North Texas for on-site line commissioning.
Connect with our technical design team today. Share your motor stack specifications, wire schedules, or target output requirements to receive a detailed line layout and engineering proposal.